Solar Structure Quality Inspection Checklist: 12 Things EPCs Should Check Before Dispatch
 Practical Notes
For an EPC contractor, receiving solar mounting structures at site is not the right time to discover incorrect hole positions, mismatched profiles, damaged coatings or missing components. Many of these issues can be identified before the material leaves the manufacturing facility.
A structured solar structure quality inspection helps EPC, procurement and quality teams verify that the supplied module mounting structure matches the approved project requirements before dispatch. The inspection should cover much more than the visible appearance of C purlins, HAT sections, rafters or other structural members. Drawings, material traceability, dimensions, thickness, coating, punching, hardware, quantities and quality records all matter.
Pre-dispatch inspection becomes especially important on repetitive and utility-scale solar projects because a manufacturing deviation can be repeated across a large batch of components.
The objective is simple: verify conformity before the material reaches site and becomes an erection problem.
The following 12-point checklist covers the key areas EPC teams should review during a pre-dispatch inspection of solar module mounting structure components.
1. Confirm the Approved Drawing, BOM and Latest Revision
Solar structure inspection should begin with documents, not with a measuring instrument.
The inspection team first needs to establish which drawings and specifications represent the approved manufacturing requirement. Depending on the project, the controlling documents may include:
- Approved fabrication drawings
- General arrangement drawings
- Bill of Materials (BOM) or BOQ
- Purchase order and technical specification
- Approved Quality Assurance Plan (QAP), where applicable
- Inspection and Test Plan (ITP), where applicable
- Approved drawing revisions and change notices
This matters because a component can be manufactured accurately and still be incorrect for the project if production was based on an outdated drawing.
The drawing revision used for inspection should therefore match the latest revision formally released for manufacturing.
EPC check: Confirm the drawing number, revision number, BOM and applicable technical specification before physical inspection begins.
2. Verify Material Grade and Material Test Certificates
A profile can have the correct shape and dimensions while still being manufactured from material that does not match the project requirement.
The EPC team or inspection agency should verify the supplied material against the approved specification and supporting material documentation.
Depending on the project requirements, this may include checking:
- Specified material grade
- Mechanical properties required by the project
- Coil or raw-material identification
- Material Test Certificate (MTC)
- Heat, batch or coil traceability where required
- Chemical and mechanical test results where applicable
- Material manufacturer or supplier identification
Indian Standard IS 2062 covers hot-rolled medium and high-tensile structural steel for structural work, but it should not automatically be assigned to every solar structure component. The applicable material standard and grade should come from the approved project specification.
EPC check: Do not rely only on broad descriptions such as “GI steel” or “high-strength steel” when the purchase order or approved specification requires a defined material grade.
3. Check Profile Dimensions Against the Approved Drawing
A solar module mounting structure can contain several different cold-formed and fabricated profiles.
Depending on the design, these may include:
- C sections
- HAT sections
- Z sections
- Columns or posts
- Rafters
- Bracing members
- Cleats
- Connection plates
For a cold-formed section, dimensional inspection may include the web, flange, lip, overall profile geometry and member length.
The component should be compared with the approved project drawing and applicable project tolerance, not with a generic purlin size chart.
This is particularly important for repetitive profiles because an incorrect roll-forming setup can affect an entire production batch.
Shree Deepak Industries manufactures galvanized C purlins in different thicknesses and project-specific dimensions. For solar applications, the final profile dimensions should be checked against the approved MMS drawing.
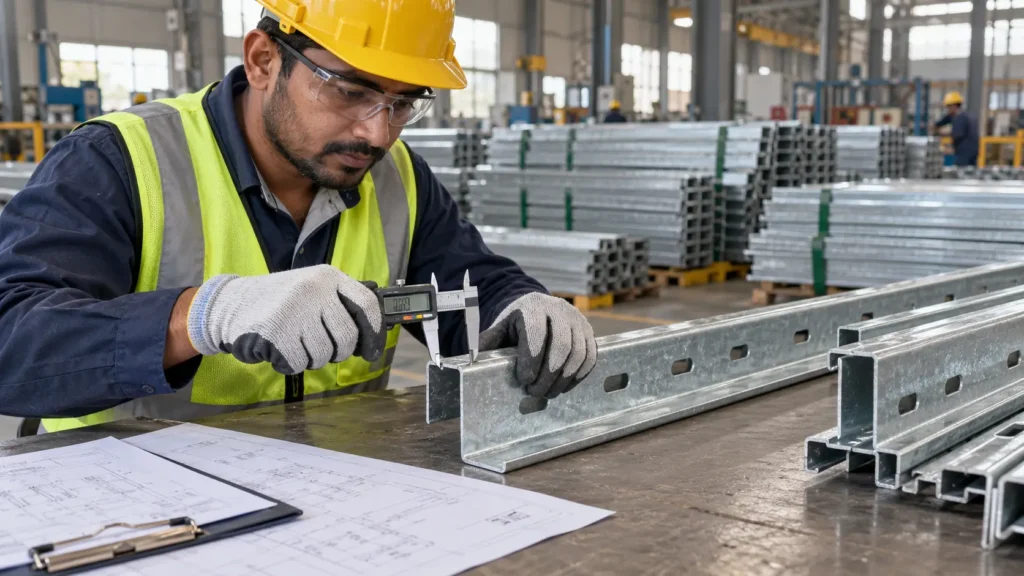
EPC check: Measure representative samples from the applicable production lot and compare the complete profile geometry with the approved drawing.
4. Verify Actual Material Thickness
Correct profile dimensions alone do not confirm that the required material thickness has been supplied.
Thickness should be measured using an appropriate calibrated instrument at the locations and sampling frequency defined by the applicable QAP, ITP or inspection procedure.
The measured value should then be compared with the material specification and applicable tolerance.
This is also why EPC teams should be cautious with generic claims such as “2 mm is the ideal solar structure thickness.” There is no single thickness that is correct for every module mounting structure.
The required thickness depends on factors such as:
- Section geometry
- Material properties
- Structural design
- Loads
- Member span
- Support conditions
- Connection arrangement
EPC check: Compare measured thickness with the approved drawing and material specification rather than a generic solar MMS thickness recommendation.
5. Inspect Hole Diameter, Pitch, Slots and Punching Accuracy
Punching is one of the most practical areas to verify before dispatch.
Solar mounting structures frequently depend on pre-punched holes and slots so that components can be connected efficiently during site erection.
Depending on the drawing, inspection may include:
- Hole diameter
- Hole-to-hole pitch
- Hole location
- Slot length and width
- Slot orientation
- Edge distance
- Connection pattern
- Alignment between mating components
- Burrs or deformation around punched areas
A member can have the correct profile and length but still create installation problems if the punching pattern is wrong.
When the same connection is repeated across hundreds or thousands of components, even a small punching error can become a recurring site issue.
EPC check: Select samples from the applicable production lots or bundles rather than checking only one specially prepared component.
6. Check Straightness, Twist, Bow and Profile Formation
Cold-formed solar structure members should also be visually and dimensionally checked for their overall shape and condition.
Inspection may look for:
- Bow
- Twist
- Local deformation
- Distorted flanges or lips
- Inconsistent bends
- Damaged edges
- Cracks
- Sharp or excessive burrs
- Handling damage
The acceptable limits should come from the approved project specification, fabrication drawing, applicable standard or agreed inspection procedure. Arbitrary universal tolerances should not be applied to every solar structure.
Profile consistency is particularly important in repetitive MMS production because variations can make alignment and assembly more difficult at site.
EPC check: Inspect samples from different bundles and production lots for consistent profile formation and acceptable straightness.
7. Verify Galvanizing or the Specified Protective Coating
Solar mounting structures operate outdoors, making corrosion protection an important part of pre-dispatch inspection.
The exact inspection method depends on the coating system specified for the project.
For example, IS 277 covers galvanized steel strips and sheets, while IS 4759 covers hot-dip zinc coatings on structural steel and other allied products. These standards relate to different product and coating routes and should not be treated as interchangeable requirements for every solar structure component.
Depending on the approved specification, coating inspection may include:
- Specified coating type
- Required coating mass or coating thickness
- Relevant coating certificates or test reports
- Measurement results where applicable
- Coating uniformity
- Bare or uncoated areas
- Peeling or flaking
- Visible surface damage
- Condition around cut or fabricated areas
- Approved repair or touch-up treatment where applicable
The inspection team should distinguish between the thickness of the steel substrate and the thickness or mass of the protective coating. They are different quality parameters.
EPC check: Ask what coating was specified, how conformity was verified and whether the inspection result satisfies the applicable project requirement.
8. Inspect Welded or Fabricated Connections Where Applicable
Not every solar MMS design contains welded components. Welding should therefore be inspected where it is actually part of the approved structure rather than treated as a universal requirement.
Where the design contains welded brackets, cleats, base plates or other fabricated assemblies, checks may include:
- Weld location
- Specified weld size
- Visible weld discontinuities
- Excessive spatter
- Distortion after welding
- Condition of the protective coating around fabricated areas
- Required welding records
- NDT results where specifically required by the QAP or project specification
Acceptance criteria should come from the approved drawing, applicable welding requirement and project QAP.
EPC check: Do not demand welding or NDT requirements that are not part of the approved design, but where welding is specified, verify it against the applicable acceptance criteria.
9. Check Fasteners, Nuts, Washers and Other Hardware
A solar structure dispatch is not complete simply because the main steel profiles are ready.
The associated connection hardware should also be reconciled against the approved BOM and technical specification.
Depending on the MMS design, this can include:
- Bolts
- Nuts
- Plain or spring washers
- Module clamps
- Connection brackets
- Cleats
- Other project-specific hardware
The inspection should confirm the specified size, material or grade, finish or coating, quantity and compatibility with the intended connection where these requirements are defined by the project.
EPC check: Cross-check hardware quantities and specifications against the BOM instead of treating fasteners as a minor accessory to the main structure.
10. Perform a Sample Fit-Up or Trial Assembly Where Required
Individual dimensional measurements can confirm many parameters, but they may not reveal every assembly issue.
Where required by the QAP, purchase order or inspection plan, a sample fit-up or trial assembly can help identify problems such as:
- Misaligned holes
- Incorrect slot orientation
- Wrong mating components
- Interference between members
- Incorrect bracket configuration
- Connection mismatches
- Assembly sequence problems
This does not mean every solar project requires a complete factory assembly of the MMS.
The extent of sample assembly should follow the agreed inspection requirement. For repetitive structures, an approved sample fit-up can provide an additional check that individually inspected components work together as intended.
EPC check: Where trial assembly is part of the inspection plan, document the selected assembly and close any fit-up issues before bulk dispatch.
11. Reconcile Quantities, Part Identification and Packaging
After technical conformity has been verified, the material still needs to reach the correct project in identifiable and usable condition.
Before dispatch, the EPC or inspection team should reconcile packed quantities against the BOM, purchase order or approved dispatch schedule.
Check:
- Part identification
- Bundle identification
- Quantity per bundle
- Total dispatched quantity
- Project or lot identification where required
- Separation of different member types
- Fastener and hardware packaging
- Protection during loading and transport
- Condition of finished surfaces before loading
Clear bundle identification can make unloading, inventory reconciliation and erection sequencing easier once the material reaches the solar project site.
Shree Deepak Industries includes secure bundling and scheduled dispatch planning within its solar structure manufacturing workflow.
EPC check: Verify that the material being loaded belongs to the inspected and accepted lot and that bundle identification corresponds with the packing or dispatch list.
12. Review Inspection Records and Dispatch Release
The final stage of solar structure quality inspection is documentary closure.
Physical material may appear ready for dispatch, but required inspection records should also be complete before release.
Depending on the project, the final quality package may include:
- Approved QAP or ITP
- Material Test Certificates
- Dimensional inspection reports
- Coating or galvanizing inspection reports
- Applicable test certificates
- Sampling records
- Inspection reports
- NCR records and closure evidence
- Third-party inspection release where required
- Packing list
- Dispatch clearance or release note
If a non-conformance was raised during inspection, its status should be clear before the affected material is released.
EPC check: Confirm that required inspection records are complete and that open quality issues have been handled according to the agreed project procedure before dispatch approval.
Which Solar Structure Inspection Requirements Are Project-Specific?
One of the biggest mistakes in solar MMS inspection is turning commonly used specifications into universal rules.
Steel grade, section thickness, coating requirement, punching tolerance and sampling frequency can differ between projects. They should be verified against the documents governing the particular order.
| Inspection Parameter | Primary Reference for Verification |
| Steel or material grade | Approved material specification, PO and applicable drawing |
| Profile dimensions | Approved fabrication drawing |
| Material thickness | Drawing, material specification and applicable tolerance |
| Hole diameter, pitch and slots | Approved fabrication drawing |
| Protective coating type | Project specification and purchase requirement |
| Coating mass or thickness | Specified coating system and applicable standard |
| Weld acceptance | Approved drawing, welding requirement and QAP |
| Fastener specification | BOM and technical specification |
| Sampling frequency | Approved QAP, ITP or inspection procedure |
| Trial assembly requirement | QAP, PO or agreed inspection plan |
| Packaging and identification | PO, packing specification and dispatch requirement |
This distinction matters because a solar module mounting structure is an engineered system. Different sites, layouts, loads, material systems and project specifications can require different acceptance criteria.
Quick Solar Structure Pre-Dispatch Inspection Checklist
Before approving an MMS dispatch, EPC and quality teams should be able to answer the following 12 questions:
- Are the latest approved drawings, BOM and specifications being used?
- Does the material match the specified grade and supporting documentation?
- Do the profile dimensions match the approved drawing?
- Is the measured material thickness within the specified requirement?
- Are holes and slots correctly punched and positioned?
- Are the members acceptably formed and free from unacceptable bow, twist or damage?
- Does the protective coating comply with the applicable project requirement?
- Are welded or fabricated components acceptable where applicable?
- Do fasteners and other hardware match the approved BOM?
- Has the required sample fit-up or trial assembly been completed?
- Are quantities, bundle identification and packaging correct?
- Are required inspection records and dispatch approvals complete?
If any answer is unclear, resolving the issue at the manufacturing facility is generally more practical than discovering the same problem after the material has been unloaded at site.
Common Solar Structure Quality Inspection Mistakes
Checking Only Visual Appearance
A clean galvanized finish does not prove that the material grade, thickness, profile dimensions or punching pattern are correct. Visual inspection is useful, but it should form only one part of the inspection process.
Using Generic Tolerances
Values copied from another project or an online article should not automatically be applied to the current MMS. Acceptance should be based on the approved project requirement and applicable standard.
Checking Only One Sample
Large production runs can include multiple coils, batches or manufacturing lots. Sampling should follow the approved inspection plan and should represent the material being released.
Ignoring Documentation Until Dispatch Day
MTCs, inspection reports and other required records should be coordinated during production rather than assembled only after the material is ready to leave the factory.
Ignoring Packing and Identification
A technically correct structure can still create site delays when similar components arrive without clear bundle or part identification.
Why Pre-Dispatch Solar Structure Inspection Matters
The purpose of a pre-dispatch inspection is not simply to create another layer of paperwork. It is to identify manufacturing and supply deviations before they become site problems.
A properly planned inspection can identify:
- Material mismatches
- Incorrect profile dimensions
- Thickness deviations
- Punching and hole-alignment problems
- Coating damage or non-conformity
- Missing hardware
- Quantity discrepancies
- Incorrect part identification
- Incomplete quality documentation
Finding these issues before dispatch can support smoother material reconciliation and installation at the project site.
For EPC and procurement teams, supplier evaluation should therefore go beyond the quoted price per kilogram. The ability to work from controlled drawings, manufacture repeatable profiles, maintain relevant inspection records and prepare material correctly for dispatch also deserves attention.
Solar Structure Manufacturing and Quality Support from Shree Deepak Industries
Shree Deepak Industries, Jaipur, manufactures steel profiles for solar and industrial structural applications. Its solar structure manufacturing capabilities include C, Z and HAT profile requirements, custom profile design, precision roll forming, punching considerations, coating protection, fit-up and tolerance support, and secure packaging for dispatch.
For C-section requirements, buyers can review the company’s C Purlin range and share project-specific drawings, dimensions and specifications for requirement-based discussion.
The final material grade, profile dimensions, thickness, coating, punching pattern, tolerance and inspection criteria for any solar project should be confirmed against the approved project documents before manufacturing and dispatch.
For a solar structure requirement, EPC and procurement teams can contact Shree Deepak Industries with their drawings, specifications, quantity and delivery requirements.
Frequently Asked Questions About Solar Structure Quality Inspection
What should be checked during solar structure quality inspection?
A pre-dispatch inspection should typically review the latest approved drawings, material documentation, profile dimensions, material thickness, punching, profile formation, protective coating, applicable fabricated connections, hardware, fit-up requirements, quantities, packaging and quality records.
What documents should EPC teams check before MMS dispatch?
Depending on the project, relevant documents can include approved fabrication drawings, BOM or BOQ, purchase order, technical specifications, QAP or ITP, Material Test Certificates, dimensional inspection reports, coating reports, NCR closure records and dispatch clearance documents.
Is there one standard coating thickness for every solar mounting structure?
No. The required coating system and acceptance criteria should come from the project’s approved technical specification and applicable standard. Requirements can differ according to the material, coating route, environmental conditions and project design.
Should EPC teams ask for an MTC before dispatch?
Where material certification and traceability are required by the purchase order, QAP or project specification, the relevant Material Test Certificate should be checked against the supplied material before dispatch.
Why is punching accuracy important in solar MMS?
Solar mounting structures frequently rely on repetitive pre-punched bolted connections. Incorrect hole diameter, pitch, location or slot orientation can create alignment and assembly problems during erection.
Should every solar structure undergo a trial assembly before dispatch?
Not necessarily. Trial assembly or sample fit-up should be performed where required by the QAP, purchase order or agreed inspection plan. The appropriate inspection scope depends on the project.
What is the difference between material thickness and coating thickness?
Material thickness refers to the thickness of the steel substrate or product as defined by the applicable specification. Coating thickness or coating mass refers to the protective metallic layer applied to the steel. They are separate inspection parameters and should not be confused.
Does pre-dispatch inspection replace structural design approval?
No. Pre-dispatch inspection verifies manufactured material against approved requirements. It does not replace structural calculations, engineering approval or project-specific design verification.
Who should define the acceptance tolerances for solar structure components?
The applicable tolerances should come from the approved project drawings, technical specifications, relevant standards and agreed quality or inspection documents. They should not be selected arbitrarily during final inspection.
Why should bundle identification be checked before dispatch?
Large solar projects can contain many similar-looking components. Clear part and bundle identification helps the site team reconcile quantities, locate the correct members and organize erection more efficiently.
Share thickness + size + quantity — we’ll reply with the best option.